Discover our primary industrial purification systems and downstream integrated liquid processing equipment customized for the Cibao regional market.
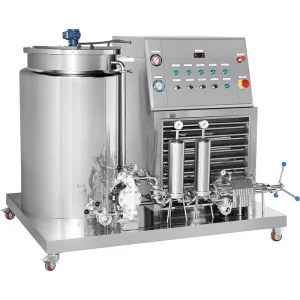
Precision fragrance chilling and membrane filtration skid designed to operate seamlessly with purified RO permeate in cosmetic manufacturing.
Explore Fragrance Chiller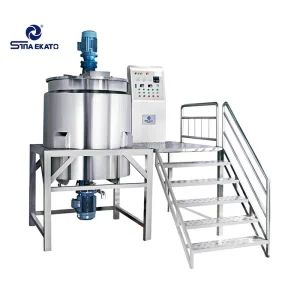
High-shear homogenizing tank for shampoo, soap, and detergent formulations utilizing low-conductivity RO purified feed water.
View Homogenizer System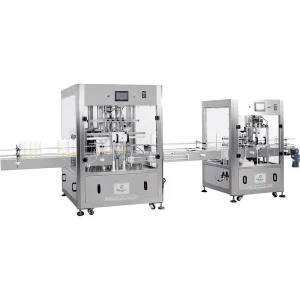
Fully integrated servo-driven filling system built with 316L stainless steel contact parts for cosmetic and personal care lines.
Inspect Filling Unit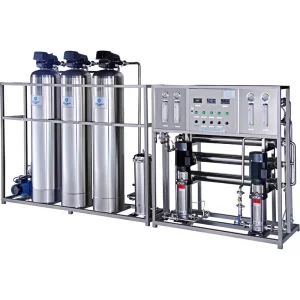
One-stage and two-stage industrial Reverse Osmosis plant with multi-media pre-treatment, quartz sand, active carbon, and EDI module.
View Industrial RO PlantA comprehensive look into raw feed water characterization, industrial park infrastructure, and membrane technology adaptation in the Dominican Republic's primary manufacturing heartland.
Santiago de los Caballeros, located in the central Cibao Valley, represents the epicenter of industrial manufacturing, garment processing, pharmaceutical production, and beverage bottling in the Dominican Republic. However, municipal and surface water supplies sourced from the Yaque del Norte River Basin and deep subterranean aquifers exhibit significant seasonal water quality fluctuations.
Key hydrological metrics recorded across Santiago industrial zones reveal Total Dissolved Solids (TDS) levels ranging between 350 mg/L to over 1,200 mg/L, accompanied by high silica content, total hardness (calcium and magnesium ions), and elevated bicarbonate alkalinity. Un-treated raw water leads to rapid scaling in boilers, catastrophic fouling of heat exchangers, and product instability in chemical and pharmaceutical formulations.
The concentration of enterprise tenants within the Víctor Espaillat Mera Industrial Free Zone and surrounding industrial corridor demands stringent process water standards. High-volume textile washing requires demineralized soft water to avoid dye color shifts; pharmaceutical facilities require USP-grade Purified Water (PW) with electrical conductivity below 1.3 µS/cm at 25°C.
SINAEKATO's RO Water Treatment Series is explicitly optimized to bridge the gap between variable municipal supply infrastructure and strict ISO/GMP manufacturing mandates across the Santiago municipal area.
How advanced modular engineering, Tier-1 international component sourcing, and optimized Chinese production yield unmatched cost-performance metrics.
Modern industrial RO plants utilize high-efficiency isobaric Energy Recovery Devices (ERD) and variable frequency drives (VFD) on high-pressure feed pumps, reducing power consumption by up to 35% compared to conventional reverse osmosis configurations.
SINAEKATO RO systems integrate 80% world-renowned brand components: Dow Filmtec / Hydranautics membranes, Grundfos vertical stainless steel pumps, Siemens PLCs, Schneider electronics, and CNP sanitary valves, ensuring long-term reliability.
All skids undergo full pressure testing, wet testing, and automated FAT (Factory Acceptance Testing) in our 10,000 m² Gaoyou production center prior to containerized shipment straight to the Port of Rio Haina or Puerto Plata.
Specific engineering implementations across key industrial sectors operating within the Cibao regional economic belt.
Scenario: Emulsification of creams, body lotions, gels, and perfumes requires water completely purged of calcium, magnesium, iron, and microbial contaminants to preserve product shelf life and clarity.
Solution: SINAEKATO Two-Stage RO System combined with UV Sterilization and 0.22 µm absolute barrier filters. Connects directly to our Vacuum Emulsifying Mixers and Perfume Chilling Machines.
Scenario: Compliance with USP and international pharmacopeia limits for Purified Water (PW) and Water for Injection (WFI).
Solution: Double-Pass Reverse Osmosis paired with Continuous Electrodeionization (CEDI) and Sanitary 316L Stainless Steel piping with orbital welding, achieving continuous resistivity >15 MΩ·cm.
Scenario: High-volume water purification requiring precise mineral balancing, ozone enrichment, and rapid bottle rinsing integration.
Solution: High-capacity 10,000L/h to 50,000L/h RO systems operating with automated ozone contact towers and CIP (Clean-in-Place) skid automation.
Scenario: Preventing scaling in thermal boilers and avoiding color fastness errors during textile dyeing processes.
Solution: Softening skids paired with Single-Stage RO systems designed for maximum recovery rates (up to 75-80%), reducing total liquid discharge.
Standard industrial models engineered for export. Custom capacities built to site requirements.
| Model Series | Permeate Output | Desalination Rate | Raw Water Feed TDS | Membrane Elements | Control Architecture | Main Frame Material |
|---|---|---|---|---|---|---|
| RO-500L | 500 Liters / Hour | ≥ 99.2% | < 2,000 ppm | Dow Filmtec 4040 x 2 | Semi-Auto / PLC Optional | SS304 / SS316L |
| RO-1000L | 1,000 Liters / Hour | ≥ 99.5% | < 2,500 ppm | Dow Filmtec 4040 x 4 | Siemens PLC + Touchscreen | SS304 / Stainless Frame |
| RO-3000L | 3,000 Liters / Hour | ≥ 99.5% | < 3,000 ppm | Hydranautics 8040 x 3 | Fully Automated HMI + Remote VFD | SS316L Sanitary Grade |
| RO-5000L | 5,000 Liters / Hour | ≥ 99.6% | < 3,500 ppm | Hydranautics 8040 x 5 | Siemens S7-1200 + SCADA Ready | SS316L / Industrial Skid |
| RO-10000L+ | 10,000 - 50,000 L/h | ≥ 99.7% | Custom Brackish / River | Multi-Array 8040 Series | Full Smart Automation + ERD | Structural SS316L Skid |
Born in 1992, SINAEKATO has grown into an international landmark machinery brand with deep expertise across mixing, homogenizing, water purification, and packaging systems.
Operating across nearly 55 countries, SINAEKATO employs around 150 skilled staff in our modern China facility and an overseas technical service team. Our long-standing commitment to quality delivers "MADE IN CHINA" excellence to blue-chip global cosmetic, pharmaceutical, and food giants.
Over 80% of our key component parts are sourced directly from world-renowned suppliers. Through multi-decadal strategic partnerships, we incorporate elite engineering components to offer users in Santiago and worldwide unmatched reliability.
Initial engagement in chemical machinery development and research.
Guangzhou Sina Cosmetics Engineering Equipment Co., Ltd. formally established.
Expansion into Gaoyou Sina Chemical Machinery & Light Industry Equipment Facilities.
10,000 m² modern plant built in Gaoyou City: SINA EKATO Chemical Machinery Co., Ltd.
Acquisition of Jingcheng and Suogao Machinery; international export expansion.
Cooperation with German FLEMAC; continuous supply of turn-key RO & liquid equipment to global markets.
Get immediate technical clarity regarding system engineering, lead times, maintenance protocols, and local installation support.
Explore our full line of perfume manufacturing, vacuum filling, labeling, sealing, and auxiliary liquid processing units.
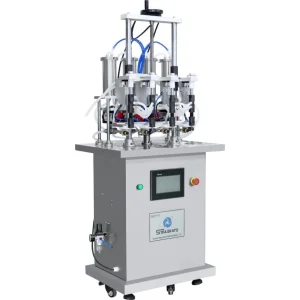
Negative pressure vacuum filling unit engineered for precise glass bottle liquid level control in fragrance packaging.
View Vacuum Filler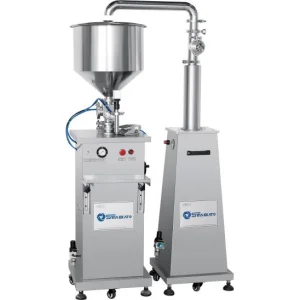
Versatile pneumatic piston filling station equipped with jacketed heating and mechanical agitation for high-viscosity products.
Inspect Semi-Auto Filler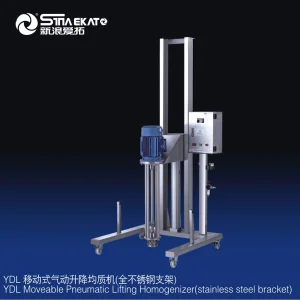
Mobile hydraulic/pneumatic lifting shear mixer for rapid particle dispersion, emulsification, and slurry mixing.
Explore High Shear Mixer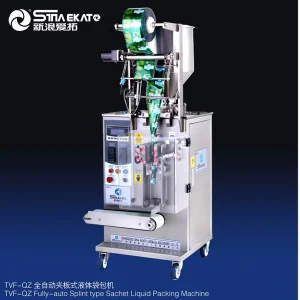
Automated sachet forming, filling, and sealing machine for single-dose cream, lotion, and shampoo sample packets.
View Sachet Machine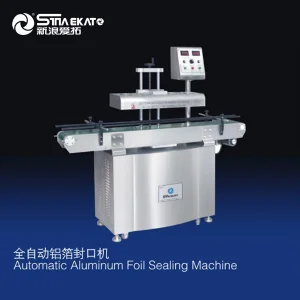
High-speed electromagnetic induction cap sealing machine guaranteeing tamper-evident, leak-proof bottle closures.
View Induction Sealer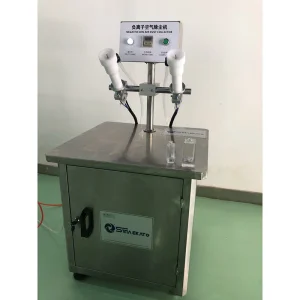
High-pressure ionized air bottle washer designed to remove dust particles prior to perfume filling.
Inspect Bottle Washer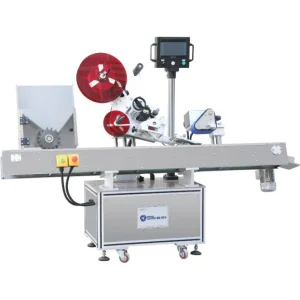
Precision self-adhesive sticker labeling machine with micro-stepping motors for front, back, or wrap-around labeling.
Explore Labeling System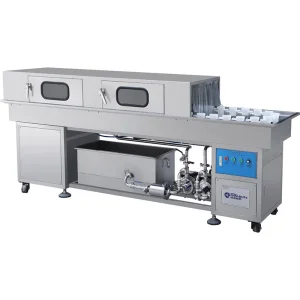
Continuous rotary water and air rinsing machine using RO purified water spray to clean beverage and pharmaceutical bottles.
View Rotary Rinser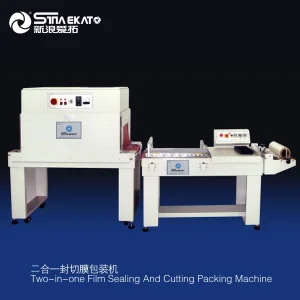
Compact semi-automatic heat shrink packaging unit for bundling secondary cosmetic and beverage containers.
Inspect Shrink Wrapper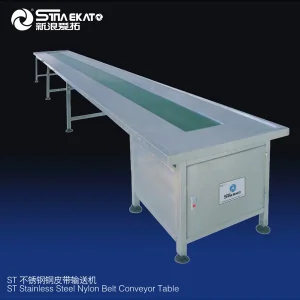
Modular industrial conveyor table with variable speed motor drive for inline product transfer between processing steps.
View Conveyor Line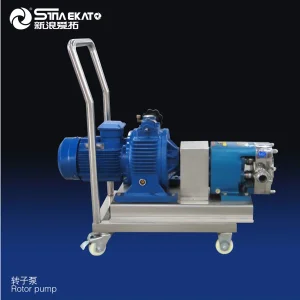
High-hygiene fluid transfer pumps built with 316L stainless steel for shear-sensitive cosmetic creams and purified liquids.
Explore Sanitary Pumps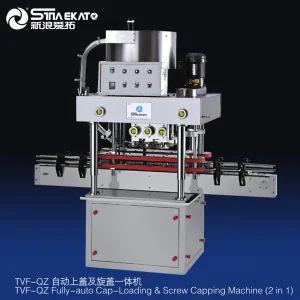
Fully automatic inline capping unit featuring magnetic torque control to eliminate cap damage on high-speed lines.
View Capping SystemContact SINAEKATO’s engineering team today for a tailored technical proposal, feed water analysis consultation, and competitive quotation.
Send Inquiry Now